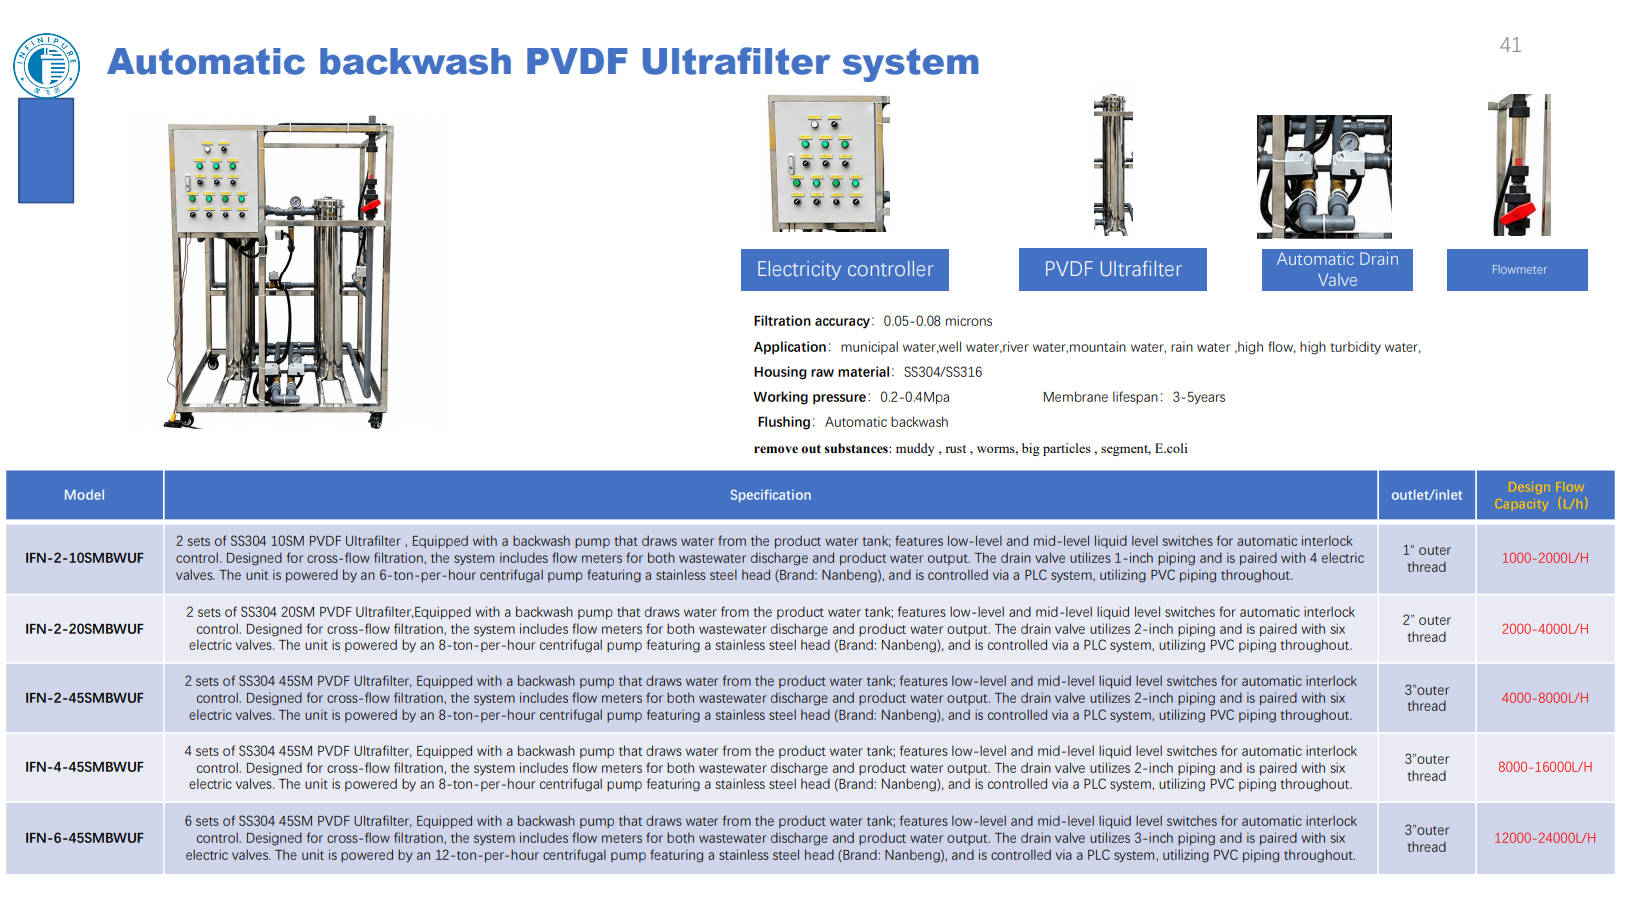
This system is designed for the advanced purification of high-turbidity, high-suspended-solids water sources. It uses high-strength hollow-fiber ultrafiltration membranes as the core filtration element. Through automatic backwash triggered by time or differential pressure, flux recovery is achieved without interrupting product water output. It can also be combined with online chemically enhanced backwash to effectively extend membrane life and ensure long-term, stable delivery of high-quality product water.
🔧 System Components
The complete automatic backwash ultrafiltration system consists of the following core units:
Ultrafiltration Membrane Modules: Made of PVDF hollow-fiber membranes with high hydrophilicity and high fouling resistance, filtration precision of 0.05–0.08 μm, and uniform pore size.
Membrane Housings and Skid Frame: Sanitary-grade housings, stainless steel or anti-corrosion carbon steel skid structure, highly integrated with a small footprint.
Backwash Unit: Consists of a backwash pump, a backwash tank (using product water), and associated piping/valves, providing high-flow reverse flushing to quickly expel contaminants from the membrane pores.
Chemically Enhanced Backwash (CEB) System: Dosing pumps and chemical storage tanks enable timed or on-demand addition of acids, alkalis, sodium hypochlorite, etc., for chemically enhanced backwash to thoroughly restore membrane performance.
Intelligent Control Center: PLC-based automatic control system with a touch screen, integrating differential pressure detection and flow monitoring. It can fully automatically switch between filtration, backwash, forward flush, chemical cleaning, and other sequences, with remote monitoring capability.
Automatic Valve Set: Pneumatic or electric butterfly valves and ball valves for fast, precise switching, ensuring automatic redirection of water flow.
Auxiliary Piping and Instrumentation: Feed and product water piping, pressure transmitters, flow meters, turbidity meters, etc., enabling real-time monitoring of system parameters.
🎯 Core Applications
Widely used in scenarios with strict product water quality requirements and fluctuating raw water quality:
Drinking Water Advanced Treatment: Removes bacteria, viruses, and colloids to ensure safe water supply.
Reverse Osmosis (RO) Pretreatment: Reduces feed water SDI, protects RO membranes, extends cleaning intervals and membrane life — the best partner for RO systems.
Industrial Feed and Process Water: Pre-treatment for high-purity water production in industries such as electronics, chemicals, and pharmaceuticals.
Municipal and Industrial Wastewater Reuse: Advanced treatment of compliant effluent for graded water reuse.
Surface and Groundwater Purification: Purification of river, lake, and well water, replacing traditional sand filters with superior product water quality.
Seawater Desalination Pretreatment: Efficiently removes suspended solids and colloids, ensuring stable operation of seawater RO systems.
💧 What It Removes
The ultrafiltration membrane barrier physically retains the following impurities, delivering nearly sterile, turbidity-free product water:
-
Suspended solids, colloidal silica, iron and manganese oxide particulates — significantly reduces effluent turbidity (typically <0.1 NTU)
-
Bacteria, viruses, and other microorganisms — >99.99% bacterial rejection, ensuring biological safety
-
Macromolecular organics, humic substances — reduces color and disinfection by-product precursors
-
Tiny eggs, algae — eliminates biological fouling risks
Does not alter water chemistry, while retaining beneficial minerals when used for drinking water treatment.
✨ Key Benefits
Provides a Reliable Barrier: Offers the strictest protection for downstream precision systems such as RO membranes, EDI, and ion exchange resins, dramatically extending their service life.
Enables Truly Unattended Operation: PLC intelligent control fully automates filtration, backwash, and cleaning regeneration, greatly reducing manual labor intensity.
Stable and Superior Product Water Quality: Unaffected by fluctuations in feed turbidity; product SDI typically <3, turbidity <0.1 NTU, laying a solid foundation for downstream processes.
Efficient Membrane Recovery Capability: Optimized backwash and chemically enhanced backwash programs effectively control fouling, reduce the frequency of off-line chemical cleaning, and extend membrane element lifespan.
Modular and Scalable: Skid-mounted design allows flexible addition of membrane modules based on capacity demands, saving space and initial investment.

